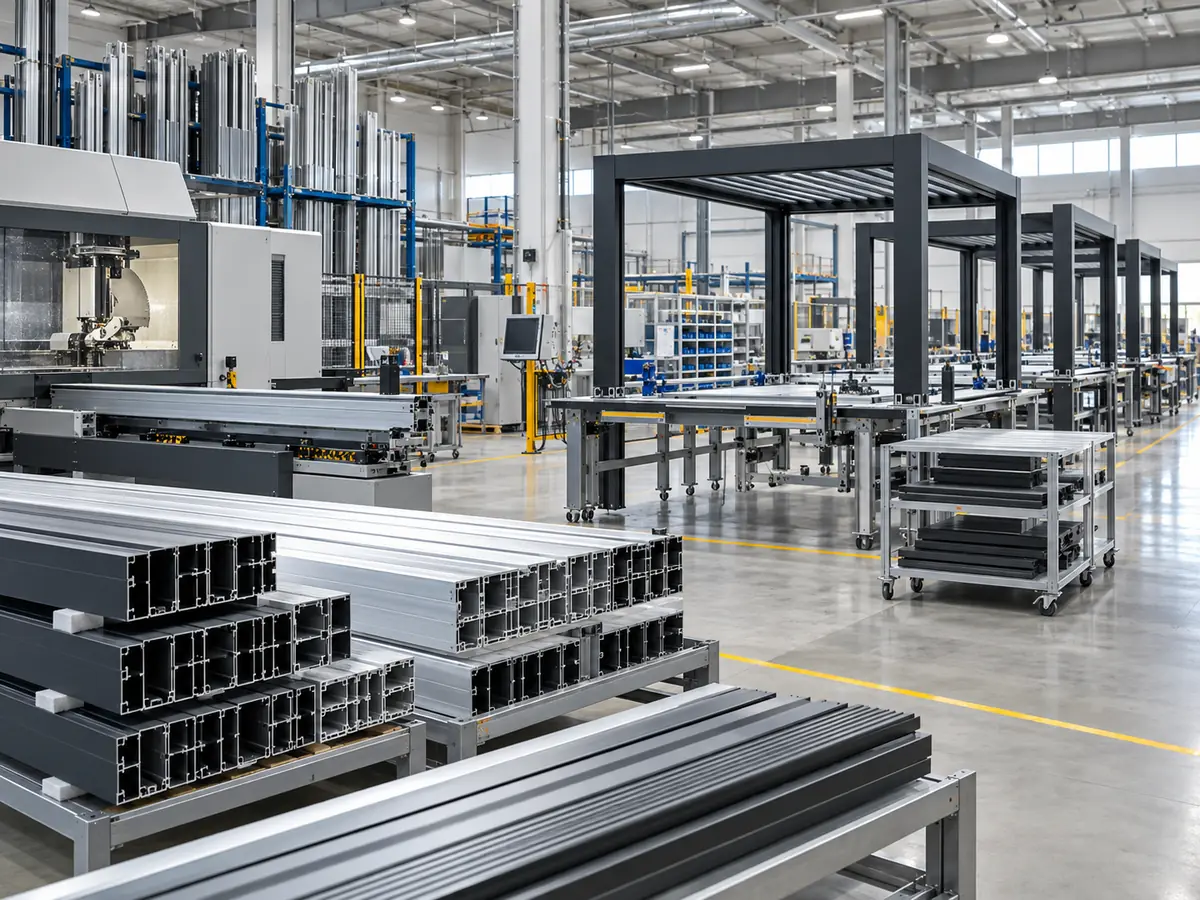
LUCY pergola quality control follows the approved project specification through profile identification, machining, visible finish, component allocation, moving-roof interfaces, drainage routes, hardware kitting and packing. The exact inspection scope depends on the selected model and order. Buyers can define required records, samples or third-party inspection before production rather than assuming a universal test package.
Best for
- Dealers evaluating repeatable product supply
- Contractors coordinating components with drawings
- Commercial buyers defining an inspection plan
- OEM programs requiring controlled revisions and labels
Key information
Key specifications
- Inspection basis
- Approved drawings, order specification and agreed finish reference
- Profile checks
- Section identity, cut length, machining and component labels
- Functional interfaces
- Roof movement, motor or manual mechanism, gutters and compatible accessories
- Packing release
- Hardware allocation, protection, labels and packing list
- Evidence boundary
- Test reports or certifications are supplied only when applicable documents are confirmed
Available options
- Buyer-defined inspection checklist
- Finish sample or agreed color reference
- Component and package photographs where agreed
- Third-party inspection discussion before order
- Nonconformity and corrective-action record where applicable
Quick comparison
| Control stage | Purpose | Buyer evidence to agree |
|---|---|---|
| Pre-production | Align drawings and specification | Approved layout, finish and options |
| In-process | Check machining and component identity | Inspection points or photographs |
| Functional review | Check selected moving interfaces | Agreed operation or subassembly record |
| Pre-shipment | Confirm allocation and packing | Packing list and inspection release |
1. Specification and drawing release
Quality control starts before cutting aluminum. The project reference should identify model, module dimensions, post positions, roof direction, drainage outlets, finish, motor or manual mechanism, control zones and selected accessories. Production and inspection should use the same approved revision.
Unresolved site information should remain open rather than being converted into a factory assumption. Local wind, snow, foundations, façade waterproofing, final electrical work and code approval remain project responsibilities unless the written scope states otherwise.
- Approved dimensioned layout
- Model and roof movement
- Finish and accessory schedule
- Drawing revision and buyer approval
2. Profiles, machining and finish
Profile identity, cut length and machining locations affect whether frames, drainage and accessories align on site. Inspection can compare prepared components with the released schedule and identify parts before packing.
Visible coating is reviewed against the agreed project reference. Exact alloy, temper, wall thickness, coating standard or test method should only be published or accepted when the corresponding LUCY technical document is available for the selected system.
| Item | Typical check | Why it matters |
|---|---|---|
| Profiles | Section and component identity | Prevents model or part mix-ups |
| Machining | Hole, slot and drainage position | Supports site alignment and water routing |
| Finish | Color reference and visible surface | Supports consistent architectural appearance |
| Labels | Module and package relationship | Simplifies receiving and installation |
3. Roof, drainage and accessory interfaces
Inspection focuses on the interfaces included in the approved configuration: frame connections, louver or retractable movement, drive or manual mechanism, perimeter gutters, selected post outlets and prepared accessory openings. A large project may be reviewed through controlled subassemblies rather than a complete full-size erection.
ZIP screens, glass, lighting, heaters and fans introduce their own mounting, electrical, clearance and operating requirements. Compatibility is confirmed for the actual opening and model; it is not inferred from a marketing photograph.
4. Pre-shipment review and records
Before shipment, hardware and controls should be allocated to identifiable packages, protected profiles should correspond to the packing list, and agreed inspection items should be closed. The buyer should define any hold point or third-party inspection before the goods are packed.
Inspection reduces avoidable mismatch but does not replace competent installation, commissioning or local approval. The receiving team should check package condition, quantities and labels before moving components to the site.
- Agreed inspection status
- Labeled hardware groups
- Packing list and package references
- Receiving and installation documents
Common questions
Does LUCY claim a zero-defect process?+
No. Quality control is a documented risk-reduction process; unsupported absolute quality claims are not used.
Can buyers arrange third-party inspection?+
Inspection timing, access and scope can be discussed before ordering and must be written into the commercial plan.
Is every pergola fully assembled before shipment?+
Not necessarily. Large systems may be checked through modules, subassemblies and critical interfaces.
Are material and certification documents available?+
Only applicable, current documents confirmed for the selected product and order should be relied upon.
Project configuration review
Discuss your pergola project with LUCY.
Share your buyer type, project location, intended use and available drawings. LUCY will route the enquiry to the relevant product, engineering or manufacturing review.
Get a quote